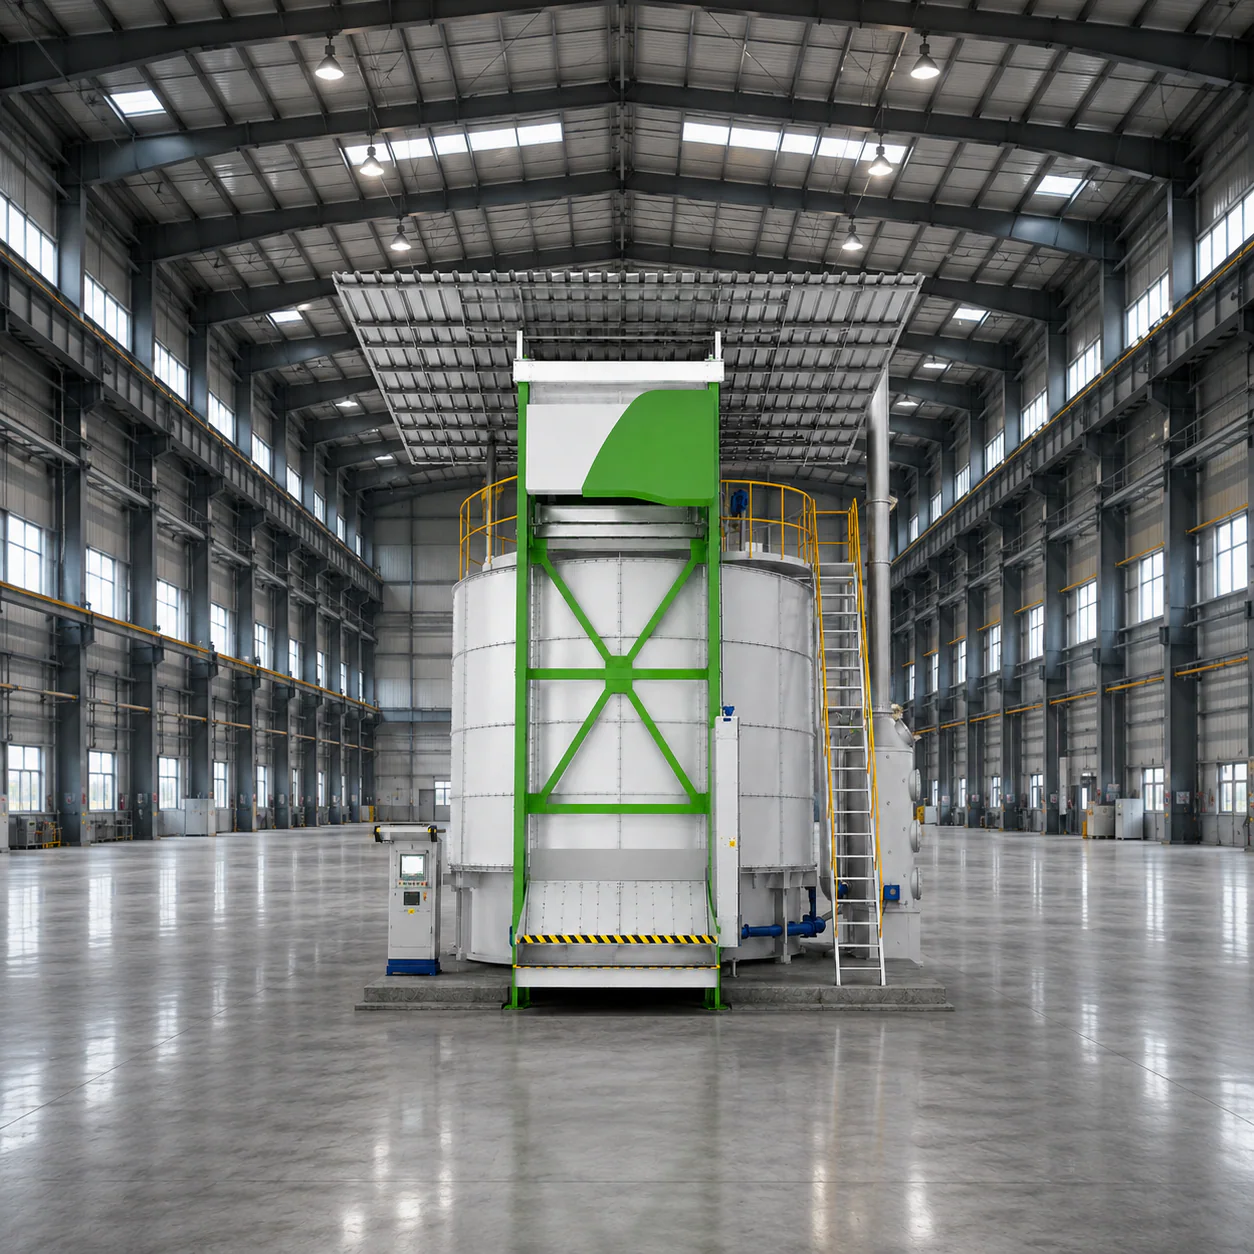
Manure extract
Soaked or pressed manure liquor. High solids; screened before the reactor.
 Get a Proposal
Ferments organic matter into a stable liquid, then filters it to a grade the drip system will accept, and holds it in tanks that keep the culture alive.
A liquid organic line is a fermentation plant, not a blending plant. The hard parts are keeping the reactor stable and filtering to a particle size the irrigation system tolerates, because a blocked drip line costs the customer more than the fertilizer.

The reactor and the filtration stage decide the product; the filling line only decides the package.
The feed determines the reactor design. High-solids feed needs separation before fermentation; sugar-rich feed ferments faster and foams more.
Soaked or pressed manure liquor. High solids; screened before the reactor.
Plant-derived liquor; lower nutrient density, higher carbon.
Carbon source and carrier; raises BOD and foaming risk.
The active component; dosing and temperature decide the shelf life.
Acid or alkali to hold the reactor in range; never added after packing.
Sold by volume with a declared analysis and, often, a live count. Consistency between batches is the commercial issue.
Typically 100–200 mesh, matched to the customer irrigation system.
N-P-K plus organic matter, per batch and per tank.
No continuing gas production in the packed container.
Declared with storage temperature; a live product changes with time.
Five stages. Fermentation and filtration carry almost all of the technical risk.
| Stage | Purpose | Key equipment | Control point |
|---|---|---|---|
| 1. Fermentation | Break down organic matter, build a stable liquor | Fermentation tank with aeration and agitation | Temperature, pH, dissolved oxygen |
| 2. Filtration | Remove solids to the irrigation grade | Screen filter and settling tank | Mesh size vs. solids load |
| 3. Blending | Adjust analysis and add micronutrients | Blending tank with agitator | Order of addition |
| 4. Storage | Hold without settling or gassing | Storage tanks with agitation | Residence time, venting |
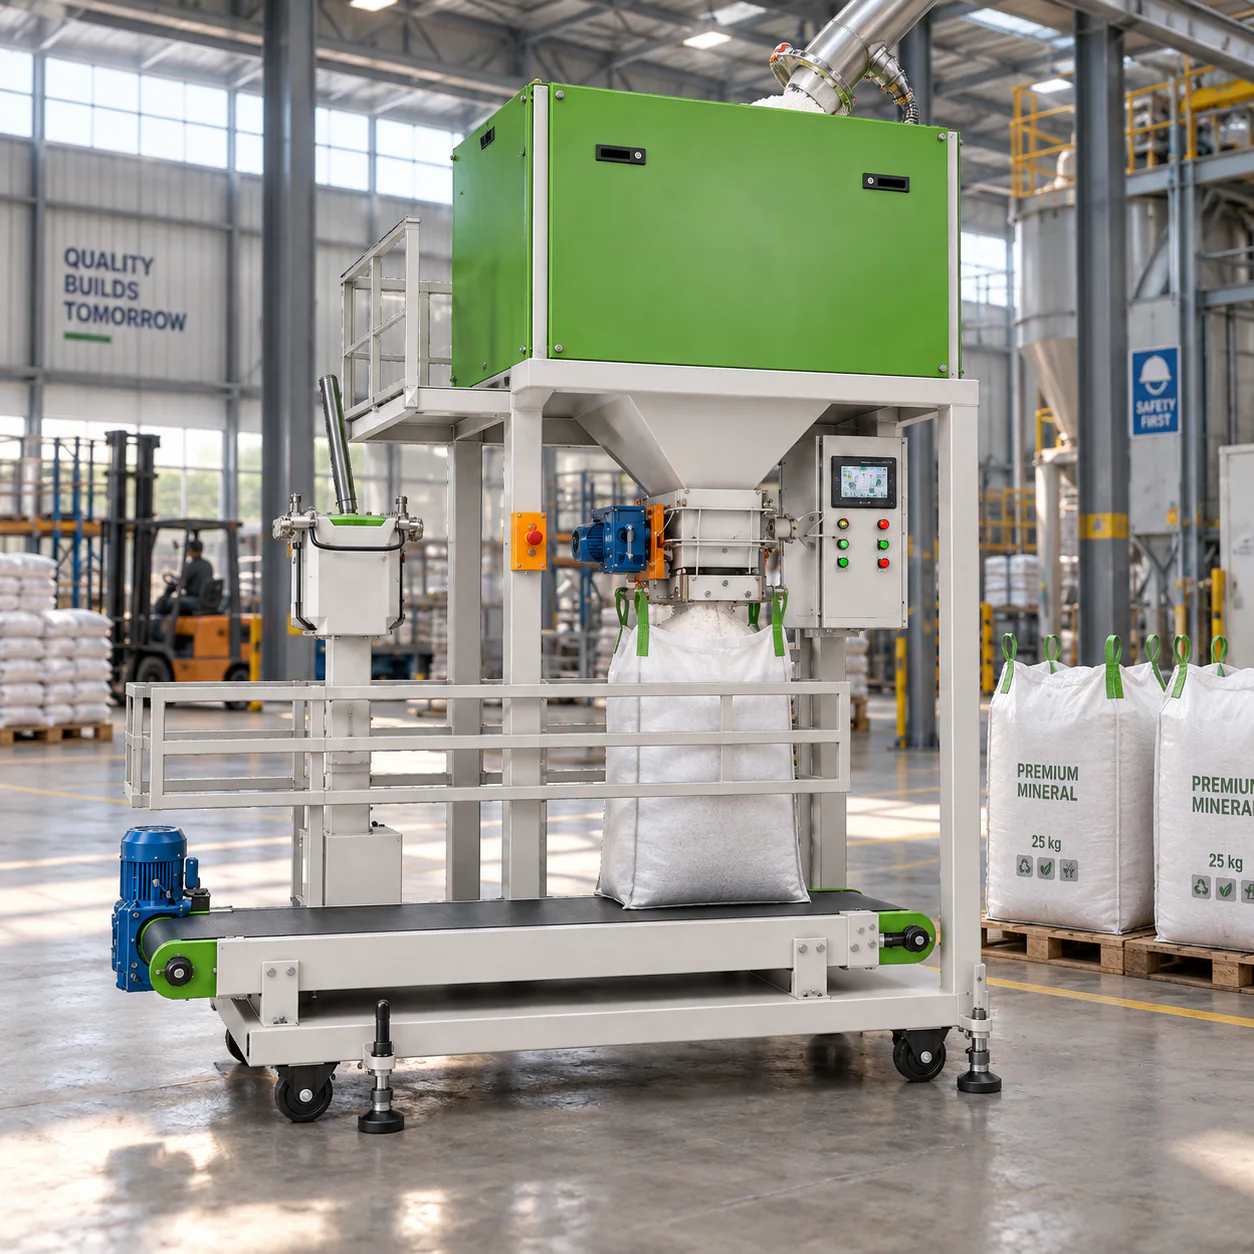
| 5. Filling | Pack to net volume | Filling machine | Fill accuracy, closure seal |
Typical equipment scope for this route. Final selection follows the approved mass balance and site conditions.
Bands describe typical project scale; the actual figure is confirmed by mass balance, not by a nominal model number.
Batch fermentation in tanks, manual filtration.
Continuous filtration and blending, semi-automatic filling.
Multi-tank plant with automated filling and storage.
Basis for the utility sheet. Local voltage, fuel and water quality are confirmed during engineering.
Agitators and aeration blowers run continuously; this is the base load.
Process water for extraction and dilution; hardness affects stability.
Aeration for aerobic routes; venting for anaerobic ones.
HDPE, FRP or stainless, chosen against the product acidity.
Controls that decide whether the line holds its specification in daily operation.
pH, temperature and DO logged; a drifting reactor produces an off-spec batch.
Checked daily; a torn screen reaches the customer drip line.
Per tank, before filling.
Leaking containers are the most common complaint on liquid lines.
Straight answers on scope, limits and what we need to quote.
Only after solids separation; the reactor cannot handle raw slurry at full strength.
Matched to the customer irrigation system, typically 100–200 mesh. Finer filtration costs throughput.
If a live count is claimed, tank temperature and storage time become part of the specification, not an afterthought.
Feed type and volume, target analysis, filtration grade, container size and site climate.
Send material, capacity and site constraints; the engineering team replies with a route recommendation.
 +8615981847286WhatsApp
 [email protected]Email
 Please enter the contentSearch
 Click to return to the topTOP